Automated Warehouses for Boxes background
Home / Warehouse Solutions / Automated Warehouses / Automated Warehouses for Boxes

Automated Warehouses for Boxes

Integrated miniload AS/RS, multi-shuttles, and goods-to-person picking systems engineered by MECALUX RACKING to maximize storage density, operational speed, and inventory control.

Engineering Excellence

Automated Storage & Retrieval Systems (AS/RS) for Totes, Cartons and Trays

MECALUX RACKING provides turnkey automated warehouse installations for light and medium unit loads. By unifying high-precision steel racking structures, automated retrieval machinery, high-speed conveyors, and proprietary Warehouse Control Software (WCS), our solutions eliminate manual travel time, reduce floor footprint by up to 85%, and ensure 24/7 picking precision.

Whether implementing a single-aisle miniload for spare parts fulfillment or a multi-shuttle high-bay distribution hub handling thousands of order lines per hour, our project engineering team designs each system according to load dimensions, weight profiles, and throughput targets.

Up to 85% Footprint Reduction vs. Static Shelving
99.99% Order Picking Accuracy
>1,000 Picks/Hour per Workstation
20+ m Vertical Clear Height Utilization
Product Architecture

Integrated Box Handling & Storage Technologies

Explore the modular components engineered by MECALUX RACKING to form complete, synchronized automated box logistics ecosystems.

Miniload stacker cranes for boxes
Miniload AS/RS

Stacker Cranes for Boxes

Fully automated single-mast or twin-mast cranes designed to navigate narrow aisles up to 20 meters high, storing and extracting boxes or trays rapidly with telescopic extractors.

Load Capacity:Up to 100 kg / unit
Max Height:20+ meters
Travel Speed:Up to 250 m/min
High speed shuttle system for boxes
High Throughput

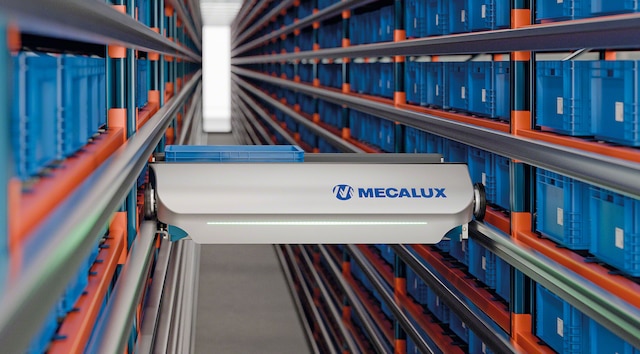
Box Shuttle System

An ultra-high-velocity multi-level storage system where autonomous shuttles operate on each level while dedicated vertical lifts transfer boxes dynamically to output pick stations.

Acceleration:Up to 5 m/s²
Configuration:Single & Double-deep
Throughput:Intensive Buffering & Picking
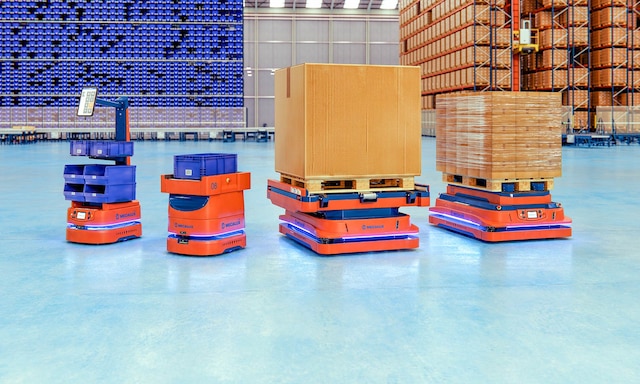
Autonomous mobile robots for tote handling
Flexible Robotics

Autonomous Mobile Robots (AMRs)

Intelligent robotic vehicles navigating freely via SLAM technology to transfer boxes and totes between storage aisles, picking tables, and consolidation dispatch zones.

Navigation:Natural Feature / SLAM
Deployment:Zero fixed guide wires
Fleet Control:Integrated Fleet Manager
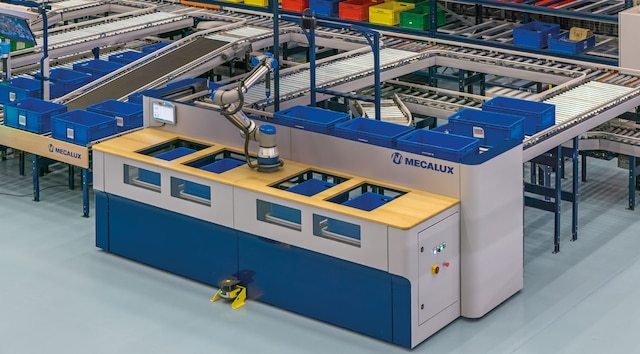
High performance pick station goods to person
Goods-to-Person

High-Performance Pick Stations

Ergonomically engineered workstations designed to present source and destination totes directly to operators, eliminating unnecessary strain and achieving high-speed throughput.

Pick Rates:Up to 1,000 picks/hour
Ergonomics:Adjustable heights & tilts
Interface:Pick-to-Light & Screen prompts
Intelligent picking robot piece picking
Robotic Piece Picking

AI Robotic Picking Cells

Advanced robotic arms equipped with 3D vision perception and smart vacuum grippers, performing autonomous piece picking and order compilation with continuous operational uptime.

Vision System:3D AI Deep Learning
Payload:Variable small items & boxes
Operation:24/7 Continuous Execution
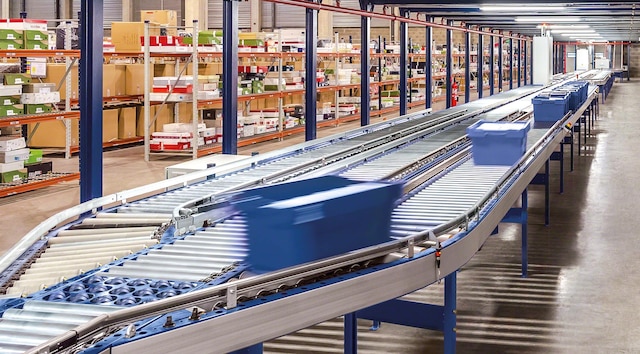
Box and carton conveyor transport networks
Internal Transport

Box & Carton Conveyor Systems

Continuous intelligent roller and belt conveyor loops, dynamic diverters, spiral lifts, and zero-pressure accumulation zones connecting storage with workstations and shipping doors.

Belt/Roller Speeds:Up to 1.5 m/s
Accumulation:Zero Pressure Accumulation
Modularity:Plug-and-play extensions
Technical Benchmarks

Comparative Performance & Engineering Matrix

Benchmark key mechanical and operational indicators across our box automation solutions to evaluate operational fit for your warehouse facility.

Solution System Unit Load Capacity Typical Height Max Operating Speed Throughput Capacity Primary Industry Fit
Miniload Stacker Crane (Single-Mast) Up to 50 kg Up to 15 m 250 m/min Medium-High (150-250 cycles/h) Spare parts, hardware, electronics
Miniload Stacker Crane (Twin-Mast) Up to 100 kg Up to 22 m 220 m/min High (Heavy payload stability) Industrial manufacturing, tools
Box Multi-Shuttle System Up to 50 kg Up to 24 m Shuttles: 4 m/s, Lifts: 5 m/s Ultra-High (800-1,200+ lines/h) E-commerce, pharma, apparel, 3PL
AMRs for Box Handling Up to 60 kg Ground to 2.5 m 1.5 m/s - 2.0 m/s Flexible / Scalable on demand Omnichannel, micro-fulfillment
Smart Carton Conveyor Network 0.5 kg - 50 kg Multi-tier routes Variable up to 90 m/min Continuous flow (up to 3,000 boxes/h) Sorting hubs, packing lines, shipping
Strategic Value

Core Advantages for Supply Chain Leaders

Why global procurement managers and intralogistics directors choose MECALUX RACKING box automation.

Maximum Cube Density

Exploit vertical clear ceiling heights up to 24 meters with ultra-compact aisle widths, releasing up to 85% of standard floor footprint for manufacturing or core processes.

Fast Goods-to-Person Delivery

Drastically shorten lead times by delivering retrieved bins and boxes directly to operator stations in sequence, supporting strict cut-off fulfillment windows.

Absolute Inventory Precision

Integrated with Easy WMS, every box movement is verified by optical scanning and weight validation, driving stock discrepancies to virtually zero.

Scalable Capital Investment

Modular racking modules, scalable shuttle fleets, and phased conveyor layouts allow supply chains to expand storage capacity as commercial demand grows.

Engineering FAQ

Technical Specifications & Procurement Considerations

Detailed answers regarding project feasibility, floor tolerance requirements, fire safety, and integration readiness.

How do Miniload stacker cranes compare to Box Shuttle systems?

Miniload stacker cranes utilize a single central mast mechanism to handle both horizontal movement along the aisle and vertical lifting across all levels, offering a highly economical solution for medium-to-high throughput operations. Box Shuttle systems install dedicated vehicles on each horizontal tier connected by high-speed end-of-aisle lifts, delivering higher combined cycle rates suitable for high-frequency e-commerce fulfillment hubs.

What unit load formats are compatible with automated box systems?

MECALUX RACKING systems are engineered to handle standard Euro-boxes (600x400 mm), custom plastic totes, corrugated cardboard cartons, and thermoformed internal trays. Load extractors can be equipped with telescopic arms, belt grippers, or side clamping forks to securely manipulate varied containers weighing between 5 kg and 100 kg.

What floor slab and civil work requirements must be met?

Automated box systems require floor slab flatness conforming to EN 15620 specifications to ensure smooth rail travel and crane stabilization at elevated heights. During the engineering design phase, our structural engineers evaluate point load capacities, dynamic anchor loads, and seismic conditions to guarantee system stability without requiring costly civil reconstruction.

How is fire protection handled inside automated high-bay box racking?

Our racking structures integrate in-rack sprinkler pipe networks compliant with NFPA 13 and EN 12845 standards. Perforated steel shelves, mesh drop-panels, and designed water distribution channels ensure sprinkler water penetrates every tier effectively while keeping automated equipment safely shielded.

How does the automated box system communicate with host ERP software?

The MECALUX RACKING control suite features Easy WCS (Warehouse Control System) and Easy WMS, which integrate seamlessly with enterprise systems such as SAP, Oracle, Microsoft Dynamics, or custom proprietary ERPs via REST APIs, web services, or certified database connectors for real-time bidirectional synchronization.

Request a Box Automation Layout & Feasibility Study

Consult with MECALUX RACKING automation engineers to assess your container dimensions, cycle volume, and available space. Receive an engineered layout design and comprehensive technical proposal.

Contact Us